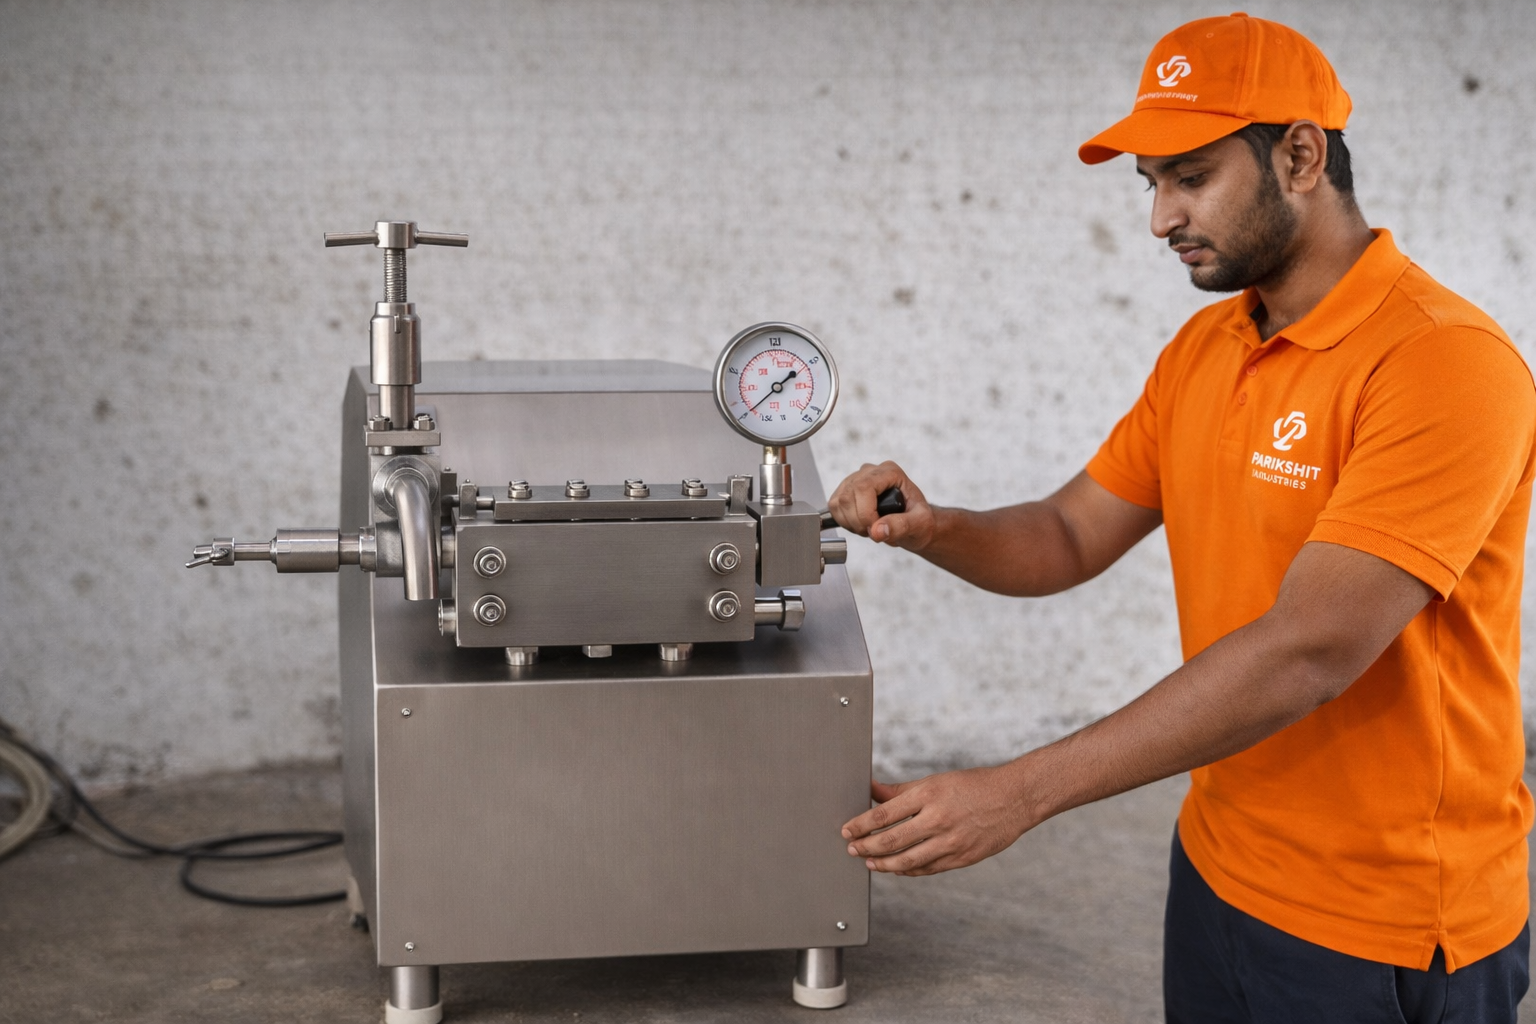
Homogenizer Supplier
In the pursuit of superior product quality and consistent performance, the role of a reliable homogenizer supplier cannot be overstated. Homogenizers are indispensable machines that refine liquid mixtures at a fundamental level, ensuring uniform particle distribution, preventing separation, and ultimately transforming textures, stability, and overall appeal across a myriad of applications. For businesses aiming to achieve excellence in their product formulations, partnering with a knowledgeable homogenizer supplier is a strategic imperative.
Understanding the Power of Homogenization
At its core, homogenization is a sophisticated process designed to reduce the size of particles within a liquid medium and disperse them evenly. This mechanical intervention is crucial for preventing ingredients from separating over time, a common challenge in many product types. By forcing liquid through a constricted space under high pressure, the homogenizer generates intense turbulence and cavitation. These forces effectively break down larger particles into much smaller, more manageable sizes, creating a stable, uniform mixture. The result is a product with improved texture, enhanced mouthfeel, greater stability, and a more consistent appearance, all of which contribute significantly to consumer satisfaction and brand reputation.
Diverse Applications Across Industries
The versatility of homogenization makes it a cornerstone technology in numerous sectors. A skilled homogenizer supplier understands these varied needs and can offer solutions tailored to specific industry demands:
Food & Beverage
This is perhaps the most prominent sector for homogenizers. In dairy, they reduce fat globule size in milk and cream, preventing separation and improving richness. For plant-based beverages, homogenizers ensure uniform dispersion of ingredients and smooth textures. They are also vital for creating stable emulsions in sauces, dressings, and flavorings, enhancing shelf life and palatability.
Pharmaceuticals
In pharmaceutical manufacturing, homogenizers are critical for creating stable suspensions and emulsions. They are used to reduce particle size for better bioavailability of active pharmaceutical ingredients (APIs), essential for injectable drugs, creams, and ointments. This leads to more effective treatments and reliable product formulations.
Cosmetics & Personal Care
The cosmetics industry relies heavily on homogenizers to produce smooth, stable lotions, creams, serums, and sunscreens. By ensuring even distribution of ingredients and preventing phase separation, homogenizers enhance product aesthetics, texture, and the efficacy of active components for better skin absorption.
Chemical Manufacturing
Beyond consumer products, homogenizers find use in creating stable mixtures for paints, coatings, adhesives, and polymer dispersions. They ensure uniform consistency and performance characteristics required in these industrial applications.
Key Benefits of Effective Homogenization
Partnering with a competent homogenizer supplier brings tangible advantages to your production process and final product:
- Improved Product Consistency: Ensures uniformity in texture, appearance, and taste batch after batch.
- Enhanced Stability: Prevents ingredient separation, extending shelf life and maintaining product integrity.
- Superior Texture & Mouthfeel: Creates smoother, richer, and more appealing product textures.
- Increased Production Efficiency: Streamlines processing by achieving desired product characteristics quickly and reliably.
- Better Ingredient Integration: Facilitates the even dispersion and potential enhancement of active ingredients.
Buyer Insight: Beyond the Machine
Selecting the right homogenizer involves more than just machine specifications. Consider the expertise of your homogenizer supplier to ensure they understand your specific product matrix, desired outcome, and operational constraints. A good supplier will guide you through critical selection factors.
Choosing the Right Homogenizer: A Buyer's Guide
As a discerning buyer, evaluating potential homogenizer suppliers and their offerings requires careful consideration of several factors to ensure optimal performance and return on investment:
Essential Selection Criteria:
- Product Characteristics: Understand your product's viscosity, solids content, and any heat sensitivity. These directly impact the type and configuration of the homogenizer needed.
- Target Particle Size: Define the desired particle size reduction for your specific application. This dictates the pressure and shear forces the machine must achieve.
- Required Throughput: Determine the volume of product you need to process per hour or day to select a homogenizer with adequate capacity.
- Material Compatibility: Ensure the materials of construction are suitable for your product, especially if dealing with corrosive substances or strict hygiene requirements.
- Operational Environment: Consider the space available and the power supply at your facility.
Questions to Ask Your Homogenizer Supplier:
- What types of homogenizers are best suited for my specific product (e.g., dairy, plant-based, emulsions)?
- What are the typical particle size reduction capabilities of your machines for my application?
- Can you provide tailored solutions for my production space and capacity needs?
- What are the maintenance requirements and typical lifespan of your homogenizers?
- What kind of support or after-sales service do you offer?
Parikshit Industries: Your Trusted Homogenizer Partner
Parikshit Industries stands as a dedicated manufacturer and supplier of essential processing machinery, including high-quality homogenizers. Located in Ahmedabad, Gujarat, India, we are committed to providing reliable solutions that meet the diverse needs of the food and beverage industry. Our expertise extends to specialized equipment like our Gelato Homogenizer, designed to enhance the quality and texture of frozen desserts. We understand the critical importance of consistent product performance and offer machinery built for efficiency and durability. Whether you require a specific solution or need guidance on the best equipment for your operation, Parikshit Industries is equipped to support your production goals with tailored solutions.
We aim to empower businesses with the processing capabilities they need to excel. Reach out to Parikshit Industries to discuss how our homogenizing equipment can elevate your product offerings and operational success.
Frequently Asked Questions
What is the primary function of a homogenizer?
A homogenizer's primary function is to reduce particle size and distribute them evenly within a liquid mixture, preventing separation and improving consistency, texture, and stability.
Which industries commonly use homogenizers?
Common industries include food and beverage (dairy, plant-based drinks), pharmaceuticals (drug delivery), cosmetics and personal care (lotions, creams), and chemical manufacturing (paints, coatings).
How does a homogenizer improve product shelf life?
By creating stable emulsions and preventing ingredient separation, homogenizers maintain product integrity over time, thereby extending shelf life.
What factors should I consider when selecting a homogenizer?
Key factors include product viscosity, desired particle size reduction, required processing capacity, material compatibility, and the available operational environment.
Elevate Your Product Quality Today
Ready to enhance the consistency, texture, and stability of your products? As a dedicated homogenizer supplier, Parikshit Industries offers the expertise and machinery to help you achieve your manufacturing goals. Contact us to learn more about our solutions and how we can support your business needs.
Contact Us Call Us